Engineering Excellence: Why Choose Our Racking Systems?
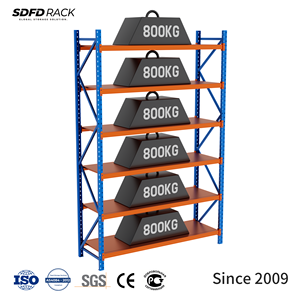
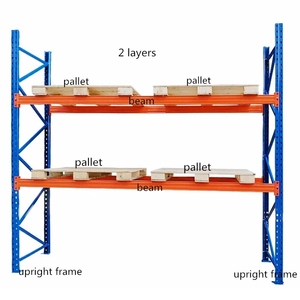
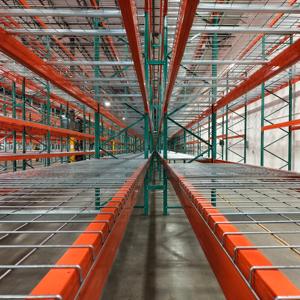
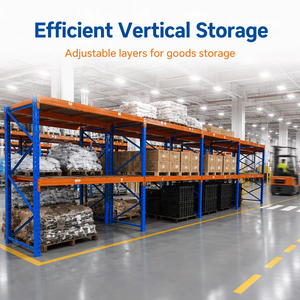
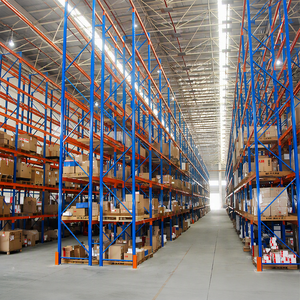
In the modern era of logistics, warehouse efficiency is synonymous with Information Gain. Our industrial pallet racking systems are not merely storage units; they are engineered assets designed for high-density, safety-compliant, and high-throughput environments. By adhering to rigorous CE Certification standards, we ensure that every bolt and beam meets the global benchmark for load capacity and seismic durability.
Future Trends in Warehouse Procurement
The transition toward "Smart Warehousing" is accelerating. Procurement trends indicate a massive shift toward modularity and automation-ready storage. Businesses are now prioritizing systems that can integrate with ASRS (Automated Storage and Retrieval Systems) and shuttle technology. Our engineering team proactively designs profiles that accommodate these future-ready integrations, ensuring your facility remains competitive over the next decade.
Industry-Leading Expertise
With decades of specialized experience in structural steel manufacturing, our company provides custom-tailored solutions for diverse industries, including cold chain, pharmaceuticals, and e-commerce distribution. Our commitment to E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) is reflected in every project, from site-specific seismic engineering to precision-guided installation support.
Common Procurement FAQs
What does CE Certification mean for my warehouse safety?
CE certification confirms that our racking systems meet European safety standards, ensuring structural integrity under designated load limits, which significantly reduces workplace accident risks.
How do I select the right racking for high-density storage?
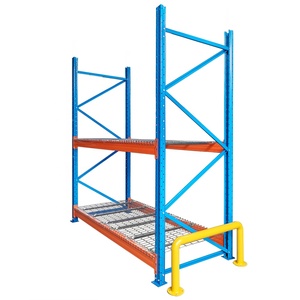
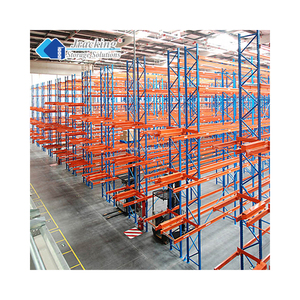
For maximum density, consider our Drive-In or Pallet Flow systems. For selectivity and speed, Selective Racking is the gold standard. Contact our engineering team for a custom CAD layout based on your SKU velocity.
Can your systems be customized for specialized goods?
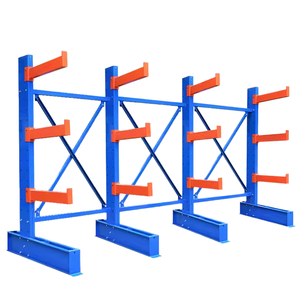
Absolutely. From cantilever racks for long materials to custom hanging sample racks, we utilize advanced fabrication to fit your unique inventory requirements.